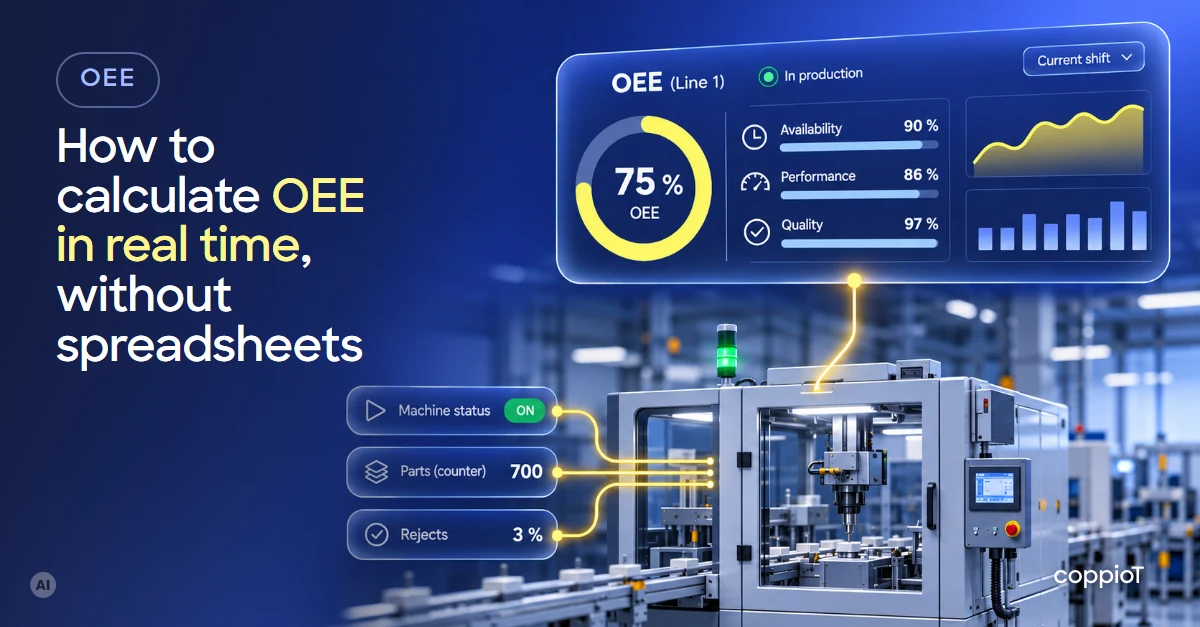
OEE¹ (Overall Equipment Effectiveness) is calculated as availability × performance × quality. It tells you how much of the planned production time made good parts at the ideal speed. To get it in real time, without spreadsheets, you only need to read three signals from the machine (running, part count and rejects) and let the calculation run on its own.
What is OEE?
OEE is the most widely used measure of how well a machine or a line is working. It comes from TPM² (Total Productive Maintenance) and was popularised by Seiichi Nakajima in the 1980s.
Its value is that it sums up, in one number, the three ways a machine loses production:
| Factor | The question it answers | The losses it captures |
|---|---|---|
| Availability | Of all the time it should have been running, how long did it run? | Breakdowns, waiting for material, changeovers, adjustments |
| Performance | While it was running, how fast did it produce compared with the ideal? | Micro-stops and slower-than-normal cycles |
| Quality | Of the parts it made, how many were good first time? | Rejects and rework |
An OEE of 100% is perfect production: no stops, at ideal speed, and not a single bad part.
OEE calculation: the formula and a worked example
OEE = Availability × Performance × Quality
- Availability = run time ÷ planned production time.
- Performance = (total parts × ideal cycle time) ÷ run time.
- Quality = good parts ÷ total parts.
An illustrative example: one 8-hour shift on a machine with an ideal cycle time of 30 seconds per part.
| Data | Value |
|---|---|
| Shift | 480 min |
| Planned breaks (meals, cleaning) | 30 min |
| Planned production time | 450 min |
| Unplanned stops (breakdown, no material, micro-stops) | 45 min |
| Run time | 405 min |
| Total parts | 700 |
| Rejected parts | 21 |
- Availability = 405 ÷ 450 = 90.0%
- Performance = (700 × 0.5 min) ÷ 405 min = 350 ÷ 405 = 86.4%
- Quality = 679 ÷ 700 = 97.0%
- OEE = 0.900 × 0.864 × 0.970 = 75.4%
A quick check: 679 good parts at 0.5 minutes each are 339.5 minutes of ideal production. Divided by the 450 planned minutes, that gives the same 75.4%.
World-class OEE: the 85% benchmark
The classic TPM benchmark puts “world-class” OEE at around 85% (roughly 90% availability, 95% performance and 99.9% quality). Many plants that measure it for the first time find themselves well below that, often around 60% (an indicative figure). Rather than comparing yourself with others, the useful thing is to watch your own line’s trend and see which factor holds it back.
Why spreadsheet OEE misleads you
Calculating OEE in a spreadsheet with hand-written data has two problems that no formula can fix.
It arrives late. If last week’s OEE is worked out on Monday, it serves the report, not today’s shift. By the time you see it, the stop is over and nobody remembers exactly why.
It hides micro-stops. Nobody writes down a two-minute stop to reposition a part. But twenty of them in a shift add up to forty minutes. And here is the trap: in the example above, if the operator only logs 25 of the 45 minutes of stops, the spreadsheet says:
| With machine data | With hand-written data | |
|---|---|---|
| Availability | 90.0% | 94.4% |
| Performance | 86.4% | 82.4% |
| Quality | 97.0% | 97.0% |
| OEE | 75.4% | 75.4% |
The overall OEE is the same, but the loss moves: the micro-stops nobody logged show up as “the machine is slow”. The team ends up checking the machine’s speed when the real problem is twenty short stops nobody sees. That is why measuring each factor correctly matters, not just the final number.
How to get real-time OEE without manual operator input
Calculating OEE automatically takes only a few signals, and almost all of them already go through the machine’s PLC³:
- Running or stopped: a status bit in the PLC (machine in cycle, in automatic, in alarm).
- Part count: the cycle or part counter the PLC already keeps.
- Rejected parts: the signal from the quality station, if there is one, or the reject counter.
- The reason for each stop (optional, but the most useful): the alarm code active when the machine stopped.
The ideal cycle time and the shifts are set once. From then on, OEE is calculated on its own, per machine, per line and per shift, and you see it as it happens. If you want to know how those signals are read, see Modbus TCP vs OPC UA.
Two caveats, so there are no surprises:
- The machine’s logic doesn’t need to change. At most, the PLC’s communication (OPC UA⁴ or Modbus⁵) has to be enabled or configured.
- The PLC holds the current values, not the history. The platform keeps the history from day one; and stop reasons come from the alarms only if the program defines them well.
OEE tracking without a PLC
It can be done too. A sensor that counts parts, wired to a pulse counter, gives you the machine’s rate; an analog input (the motor current, for example) tells you whether it is running. It is the way to go for older machines: we explain it in how to connect legacy machinery to the cloud.
How we do it with coppioT
coppioT is engapplic’s no-code industrial IoT⁶ platform: it connects your machines to the cloud, whatever their brand, with no programming needed. For OEE, the path is:
- We pick the signals for running, parts, rejects and alarms your machine already has.
- We connect them over OPC UA or Modbus through a gateway on the plant floor, whose installation files coppioT generates. If the machine has no PLC, our gateway, available on request, reads the pulse counter and the analog inputs.
- We set the ideal cycle time and the shifts.
- We build the OEE dashboard with you in Grafana or Power BI: per shift, per machine, with stops ranked by the time they cost you. You can add alerts too, for example when a machine has been stopped for more than ten minutes.
All of it in days, not months: up to 90% faster than building it by hand. We start with a short consultancy at a fixed price with engapplic and a pilot on one or two machines before scaling up. To make sure the dashboard actually gets used on the floor, read industrial dashboards that actually get used.
Frequently asked questions
How do you calculate OEE?
Multiply availability (run time ÷ planned time), performance (parts × ideal cycle time ÷ run time) and quality (good parts ÷ total parts). A shortcut that gives the same result: good parts × ideal cycle time ÷ planned production time.
What is a good OEE score?
The classic “world-class” benchmark is 85%. It is indicative: it depends a lot on the type of process. What really counts is your line’s trend and knowing which factor limits it.
How can I get real-time OEE without manual operator input?
Read running status, part count and rejects from the PLC or from sensors, and let the platform calculate OEE on its own. The operator only needs to step in if you want a stop reason the machine can’t give.
Can you track OEE on a machine without a PLC?
Yes, with a sensor that counts parts and a signal that says whether the machine is running, wired to a gateway with a pulse counter and analog inputs.
What is the difference between OEE and TEEP?
OEE is measured against planned production time; TEEP⁷ against all 24 hours of every day. TEEP tells you how much capacity is left if you add shifts; OEE, how well you use the ones you have.
Want to see your line’s OEE in real time? Ask for a demo: complete the form and we’ll show you how it would look with your machines.
Acronyms
¹ OEE (Overall Equipment Effectiveness): how much of the planned time went into making good parts at the ideal speed.
² TPM (Total Productive Maintenance): a methodology that gets production and maintenance to look after the equipment together; OEE comes from it.
³ PLC (Programmable Logic Controller): the controller that runs the machine, for example a Siemens S7 or a Beckhoff.
⁴ OPC UA (Open Platform Communications Unified Architecture): an industrial communication standard for reading data from a PLC or other equipment securely, with its name and type.
⁵ Modbus: a simple, widely used industrial communication protocol (RTU over a serial line, TCP over Ethernet). Data is read from numbered registers, following the map the equipment maker provides.
⁶ IoT (Internet of Things). Industrial IoT connects machines and plant equipment to collect their data and put it to use.
⁷ TEEP (Total Effective Equipment Performance): calculated like OEE, but against all 24 hours of every day.


